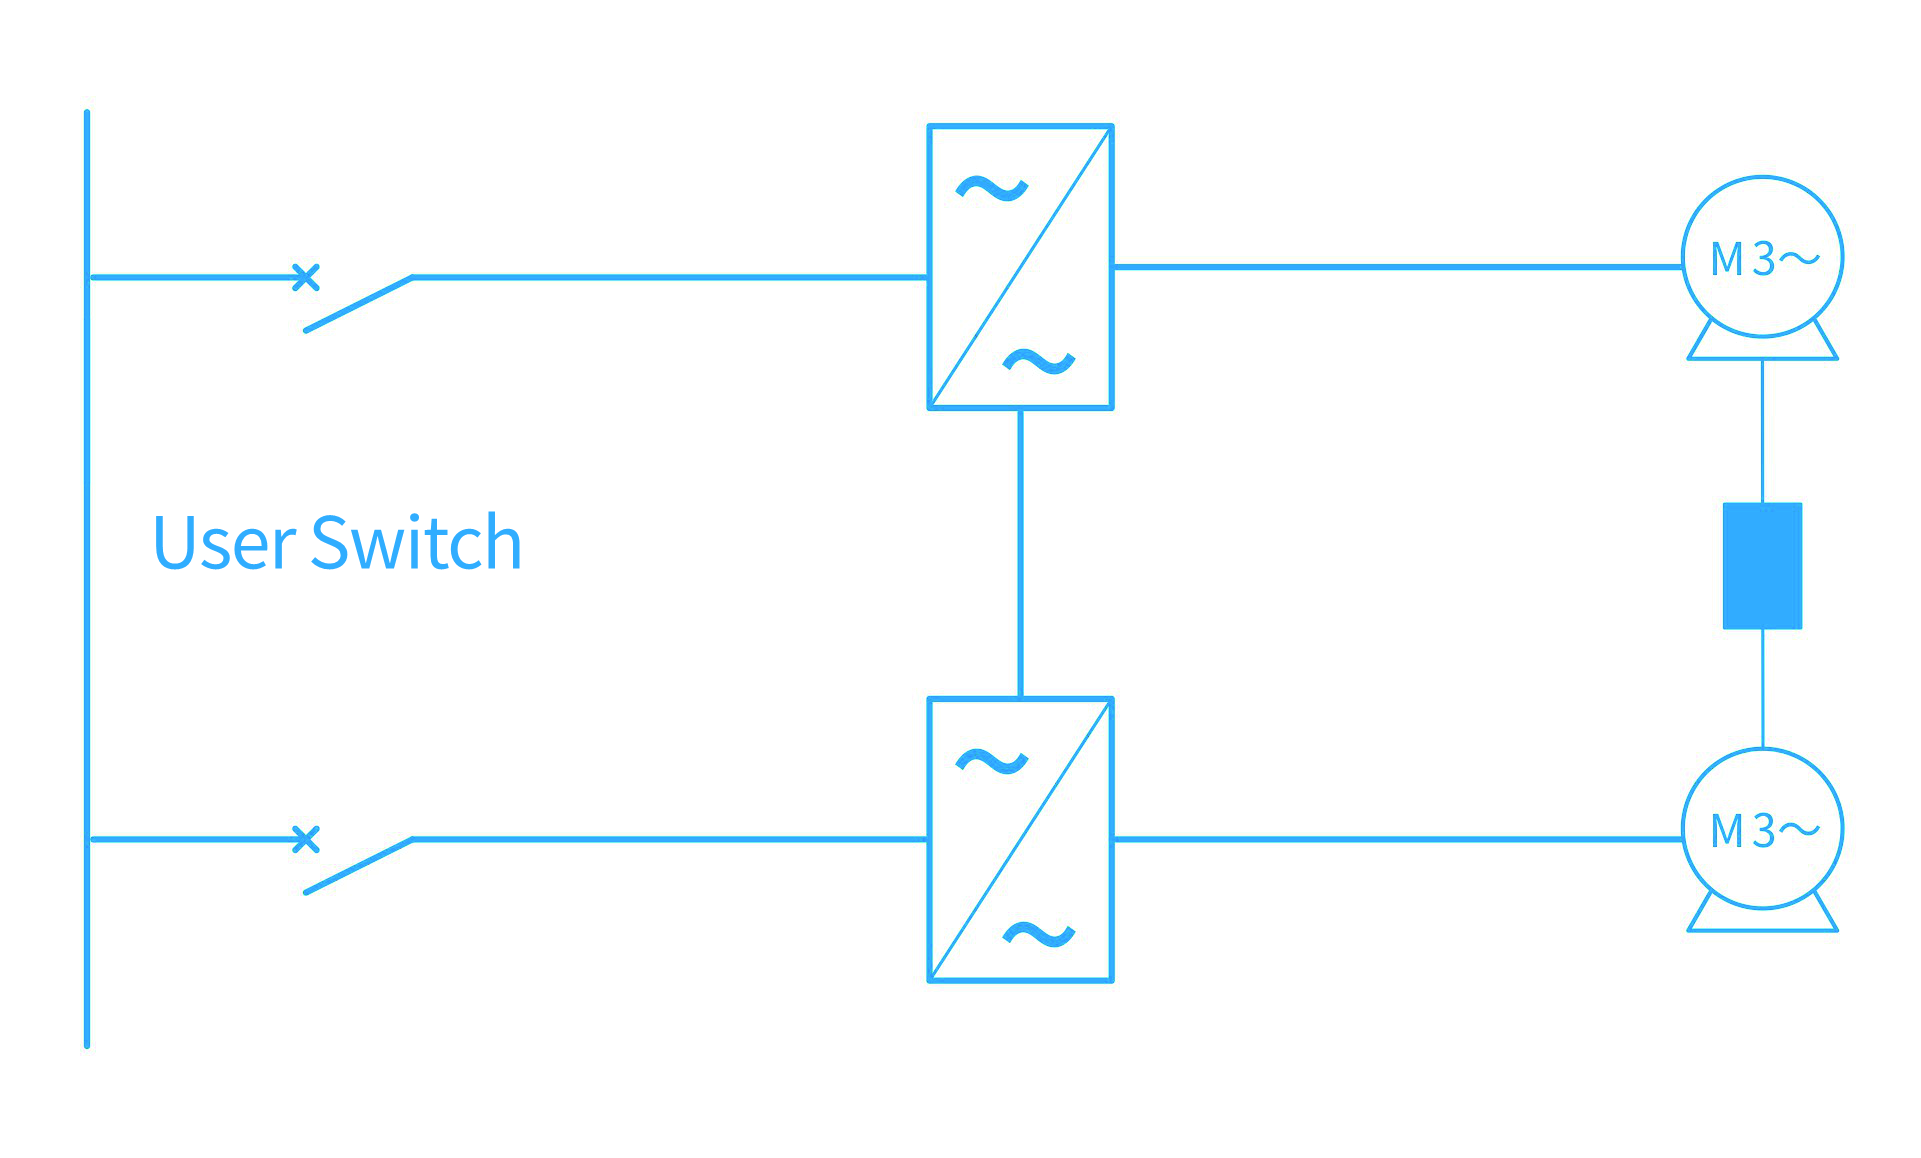
Rigidity & Flexibility in Balance: Supports multiple master-slave control modes. Torque control or droop compensation strategies can be selected for rigid and flexible connections to achieve balanced load distribution.
"Ultra-Long-Distance Fiber Optic Ring Network": Supports long-distance fiber optic communication over 6 km. The ring network ensures millisecond-level signal response, meeting the coordinated control requirements of the head and tail of ultra-long belts.
“Full-Link Safety Protection”: Integrates slip protection, belt breakage capture interlock, speed anomaly detection and STO safety torque off. It realizes millisecond-level coordination between electric braking and mechanical braking, preventing overspeed and reverse rotation.
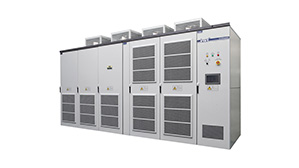
“Three-Proof & One-Durability Design”: Independent air duct + three-proof paint coating + wide-temperature components, effectively resisting dust, moisture and acid mist corrosion to extend equipment service life.
“Pre-Diagnosis”: Monitors the operating status and life attenuation trend of IGBT modules, electrolytic capacitors and cooling fans in real time, and realizes remote condition monitoring and fault diagnosis via the cloud platform.