Chemicals

Technological Innovation, Stability First INVT deeply empowers intelligent manufacturing in the chemical industry. With advanced drive technology, it builds safety barriers, ensures stable operation, unlocks energy-saving potential, and optimizes production processes, helping customers reduce energy consumption and improve efficiency.

Building a Solid Safety Barrier to Ensure Stable Production

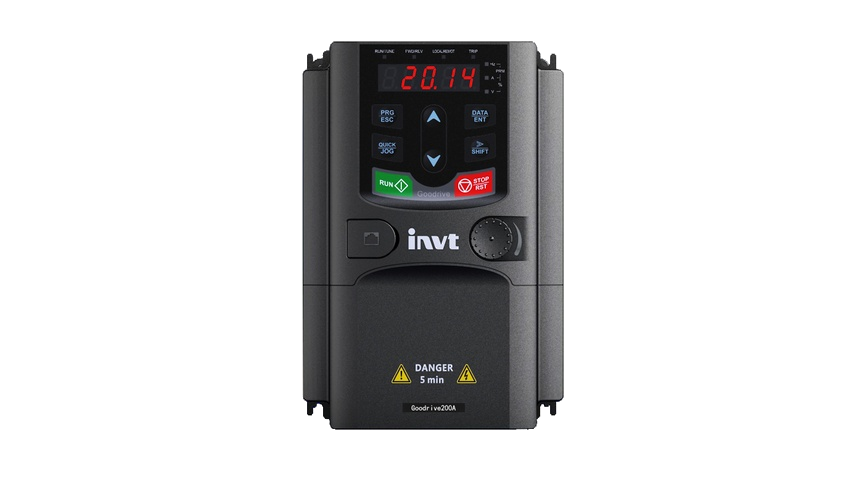
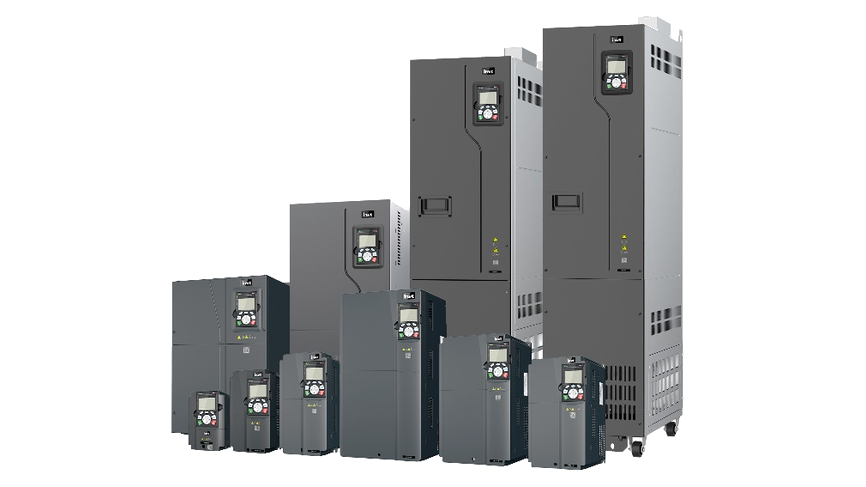
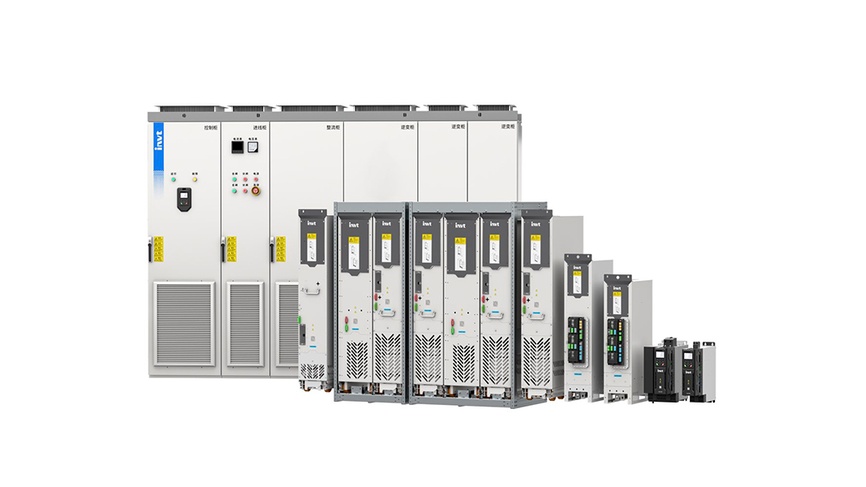
The chemical industry is one of the key pillars of the national economy, covering a wide range from basic chemicals to fine chemical products. It is characterized by continuous production, high-risk environments, high energy consumption, complex media, and stringent process requirements. These characteristics mean that inverters are not just tools for “speed regulation and energy saving,” but also critical equipment for process control and safety assurance. Through deep industry exploration, INVT not only provides engineering drives focused on stability, but has also developed a new low-voltage thermal redundancy inverter, significantly reducing the risk of equipment failure. This delivers a “safe, reliable, energy-efficient, and intelligent” drive solution for the industry.
Advancing Industry Performance with Technology

01

Redundant Safety Operation

For critical loads, a redundant parallel solution is adopted. When one inverter fails, the other seamlessly takes over without downtime, ensuring production continuity and avoiding significant losses and safety risks caused by unplanned shutdowns.

02

Stability and Reliability

Comprehensive protection functions (overcurrent, overvoltage, undervoltage, overheating, phase loss, etc.) and robust hardware protection (wide voltage design, reinforced conformal coating, IP55 enclosure, high-quality components, excellent EMC performance) meet the requirements of long-cycle, full-load operation in chemical plants.

03

Energy Saving and Consumption Reduction

For major chemical loads (pumps, fans, and other fluid applications), process-based energy saving replaces traditional valves and dampers, achieving 20%–40% energy savings. The inverter adopts an upgraded “Euler” energy-saving algorithm platform, reducing internal losses and significantly improving operating efficiency.

04

Advanced Process Control

Precise speed and torque control ensure consistency in chemical reactions and uniform product quality. Smooth acceleration curves and skip frequency functions eliminate “water hammer” in pumps and “surge” in fans, protecting pipelines, valves, and other mechanical equipment.

05

Intelligent Operation and Maintenance

Supports multiple industrial communication protocols and can be easily integrated into DCS or SCADA systems for remote centralized monitoring, reducing the need for personnel to enter hazardous areas. Combined with upper-level systems, it enables predictive maintenance by recording operational data (current, voltage, temperature, runtime) and historical faults. Data analysis helps predict potential failures, allowing maintenance to shift from reactive to proactive.

Chemicals - Core Solutions

Have questions or need support?

Our professional team is here to help.

Inquiry
TOP
We use cookies to understand how our audience uses our site.
Our site uses cookies to provide you with a better onsite experience. By continuing to browse the site you are agreeing to our use of cookies in accordance with our Cookie policy.
Accept
Reject
Cancel